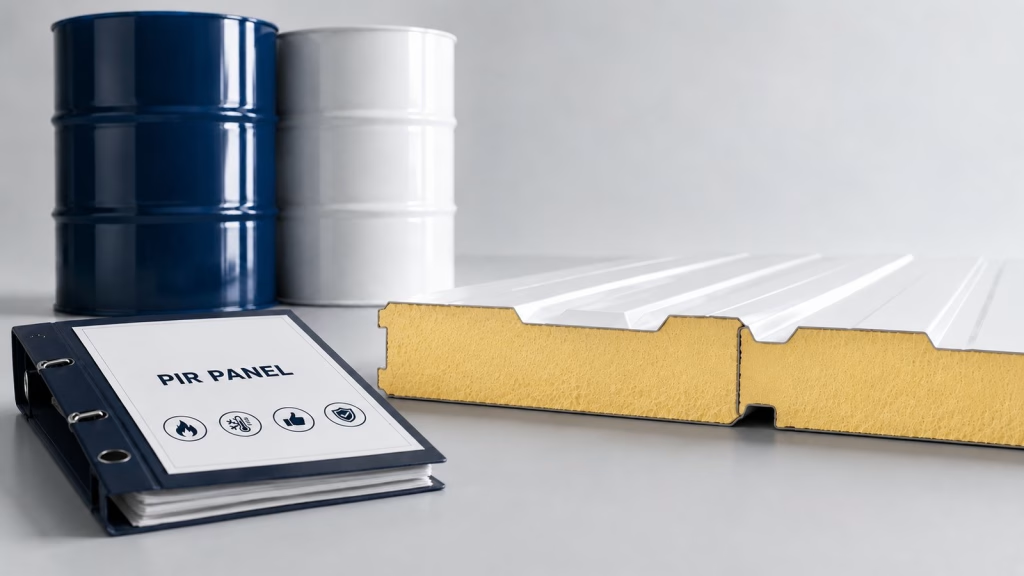
For sandwich panel manufacturers, the balance between insulation performance and fire behaviour is the most critical heading in system selection. A PIR insulation board builds that balance on different chemistry from conventional polyurethane: it reaches a better reaction-to-fire class at the same thickness without giving up much thermal performance. This article covers what PIR is, how it genuinely differs from PUR, how lambda value and fire class should be read, the five technical criteria that govern system selection, and how requirements change with the production line.
What Is a PIR Insulation Board?
PIR stands for polyisocyanurate. Like polyurethane it relies on the reaction between polyol and isocyanate, but the isocyanate is used in significant excess, and that excess creates a different chemical structure.
In a conventional rigid polyurethane (PUR) system, isocyanate is dosed to match the hydroxyl groups of the polyol. In PIR systems that amount is deliberately exceeded. Once no hydroxyl groups remain to react, the surplus isocyanate reacts with itself in the presence of suitable catalysts.
How the Isocyanurate Ring Forms
Surplus isocyanate molecules combine in groups of three to form a closed ring structure. That structure is the isocyanurate ring, and every characteristic behaviour of a PIR insulation board derives from it.
The ring is thermally far more stable than a linear urethane bond. It does not break down easily at elevated temperature; instead it forms a carbonaceous layer, known as char, on the surface, slowing the advance of flame into the material. The difference in fire performance comes precisely from this mechanism.
Two conditions are required for this reaction: sufficient isocyanate excess and a trimerisation catalyst. A PIR system is therefore not simply “a PUR recipe with more isocyanate” – the catalyst package must be designed around that structure as well.
The Real Differences Between PIR and PUR
On the shop floor the two systems are often used interchangeably. In reality the differences are measurable and they affect production decisions directly.
- Reaction to fire: At equal thickness PIR generally achieves a better class; char formation slows flame spread,
- Thermal stability: PIR deforms less at elevated temperature and holds dimensional stability longer,
- Friability: The isocyanurate ring is a rigid structure; PIR can be more brittle than PUR and generates more dust during cutting,
- Adhesion: Surface friability can weaken the bond to the metal facing; the formulation has to compensate,
- Processing window: The PIR reaction is more temperature sensitive than PUR; mould and component temperatures must be held in a narrow band,
- Cost: Because more isocyanate is consumed, raw material cost is generally higher.
This comparison makes one thing clear: PIR is not automatically the right choice in every case. In a cold room panel with no mandatory fire class requirement, a well-formulated PUR system may be more advantageous in processing ease and adhesion. The decision starts with the building regulation applying to the structure where the panel will be used.
Thermal Performance: Lambda Value and Insulation Thickness
Thermal conductivity, expressed as lambda, sits at the centre of the panel sales argument. Rigid PU and PIR foams hold one of the lowest lambda values among insulation materials thanks to the blowing gas trapped in their cells.
The point to note is that the lambda value of PIR can be slightly higher than that of PUR. While the isocyanurate structure brings fire performance, cell structure and gas retention behaviour shift somewhat. Choosing PIR therefore does not mean “better fire and better insulation” at once; a balance is struck.
Declared Value or Aged Value?
This is the critical distinction to clarify when asking for a lambda value. The blowing gas in the cells is partly replaced by air over time, and the lambda value rises somewhat.
There is therefore a difference between the initial value measured on a fresh sample and the value after ageing. Insulation thickness calculations must be based on the aged value; otherwise the project calculation will not hold in the field. The technical data sheet from the supplier is expected to state this distinction explicitly.
Reaction-to-Fire Classes and Regulatory Compliance
In Europe the reaction-to-fire class of construction products is determined according to EN 13501-1. The classification is not a single letter but three components: the main class (B, for example), smoke production (s) and flaming droplets (d).
The most common mistake appears right here: the class is awarded to the panel system, not to the foam. The same PIR foam can produce a different result with a different facing material, a different thickness or a different joint detail. The configuration a supplier’s certificate actually covers must therefore always be checked: which metal thickness, which panel thickness, which joint detail.
For industry resources on PU and PIR insulation practice in the European market, the publications of PU Europe are a useful reference.
Five Technical Criteria for Selecting a PIR System
When evaluating a PIR insulation board system, price is only one input. The five headings below determine how the system will behave on the line and in the field.
1. Isocyanate Index and Catalyst Package
The index is the percentage of isocyanate actually used relative to the theoretically required amount. In PUR systems this is held at the level needed to form urethane bonds; in PIR systems it is raised markedly.
Raising the index alone does not produce PIR, however. Without a trimerisation catalyst the surplus isocyanate does not convert into ring structures, and what you obtain is not PIR but an unnecessarily hard and brittle PUR foam. The supplier should confirm both the target index range and that the catalyst system is designed for that index.
2. Reactivity Profile and Line Speed Match
Cream time, gel time and free rise density determine whether the system suits your line. On a continuous lamination line reactivity is tuned to belt speed; if the system gels too quickly the reaction advances before the cavity is filled, and if it is too slow the panel lacks sufficient hardness at the press exit.
The mould and component temperature at which these values were measured must always be asked. A reactivity figure obtained under laboratory conditions will not reproduce on a line running at a different temperature.
3. The Balance Between Adhesion and Friability
Friability is the best known weak point of PIR foam. In an adhesion test the failure should occur within the foam itself; if it occurs at the interface between foam and metal facing, the bond is inadequate.
A well-formulated PIR system includes additives that balance adhesion while preserving the fire performance the isocyanurate structure provides. Taking a section from a sample and examining the failure surface is more informative than the numbers on a technical data sheet.
4. The Scope of the Fire Certificate
The existence of a certificate is not enough; its scope matters. Which panel thickness, which facing material and which test standard it was issued for must be checked. If your production range falls outside the configuration on the certificate, the document does not cover those products.
5. Supply Consistency and Documentation
Because PIR systems operate within a narrow processing window, they are more sensitive to batch-to-batch deviation than PUR. Requesting a certificate of analysis per shipment is far more reliable than trusting catalogue values. The criteria in our article on Polyol Supplier Selection apply to these systems as well.
Quality Control: What to Check on the Line
Even the right system produces deviation if it is not monitored. A few simple checks catch most problems before they reach the customer.
- Reactivity on site: Cream and gel times measured at actual component temperature, not the laboratory figure,
- Core density: Measured on a section cut from the panel, compared against free rise density,
- Cell structure: Examined visually on the section; fine and regular cells with no voids at the edges,
- Adhesion: Failure should occur within the foam, not at the facing interface,
- Dimensional stability: Samples held at hot and cold conditions and measured for dimensional change.
Recording these five values per batch turns a quality dispute months later into a traceable question rather than a guess.
PIR on Continuous and Discontinuous Lines
The production method directly affects PIR system selection.
On continuous lines the foam is poured between two moving metal facings and reacts along the laminator. What matters here is the match between reactivity and belt speed, and flow behaviour that leaves no marking on the facing. System options are listed on our Continuous and Discontinuous Panel Polyurethane Raw Materials page.
On discontinuous presses mould filling time and flow behaviour take priority. The cavity must fill completely, no voids may remain at the corners, and press time must match the cure speed of the system. For applications such as cold room panels, our Discontinuous Panel and Cold Room Panel Systems page completes the picture.
In both methods the adhesives used at panel joint details are a separate heading; our Sandwich Panel Adhesives page covers separate solutions for EPS, rock wool and PIR.
Common Mistakes
- Treating PIR as superior in every case: Without a fire requirement, PUR can be more suitable for processing ease and adhesion,
- Raising the index without changing the catalyst: No ring structure forms, only a brittle foam results,
- Accepting a lambda value without asking about ageing: Project thickness calculations will not hold in the field,
- Not checking the configuration on the fire certificate: It may be valid for a different thickness or facing,
- Assessing reactivity independently of measurement temperature: This is the main cause of seasonal deviation,
- Judging adhesion by numbers alone: An assessment made without examining the failure surface is misleading.
Conclusion
A PIR insulation board forms the basis of sandwich panel applications requiring fire performance, thanks to the thermal stability and char formation the isocyanurate ring provides. That advantage is not free, however: it demands a narrower processing window, carries a higher friability risk and requires a more careful adhesion balance.
The right decision starts with the building regulation applying to the structure; index and catalyst package, reactivity profile, adhesion behaviour, certificate scope and supply consistency are then assessed together. Once these five headings are settled, production waste falls and the field performance of the panel becomes predictable.
For the complete raw material family used in panel production, see our Sandwich Panel Polyurethane Raw Materials page, and for the chemical background see our article on Polyurethane Raw Materials in Sandwich Panel Production.
Contact our technical team to identify the PIR system matched to your production line and fire class requirement.